
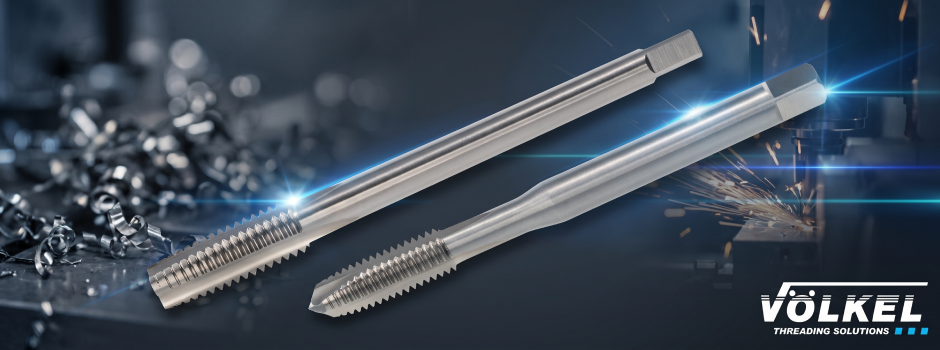
Material and Manufacturing Standards
The tool is manufactured from cobalt high-speed steel HSS-E (Co 5%), which provides superior heat resistance, wear resistance, and cutting edge stability when operating at high cutting speeds. These taps effectively handle structural, carbon, and alloy steels with tensile strength up to 900 N/mm², stainless steels, as well as non-ferrous metals.
Manufactured in accordance with DIN 371 (with a reinforced shank — for thread sizes up to M10) and DIN 376 (with a reduced/overflow shank — for thread sizes M12 and above), they guarantee rigid chuck clamping and high positioning accuracy during deep thread cutting.
What Is the Difference Between Form A and Form B?
Both versions are engineered for through-holes, where chips are evacuated forward in the direction of cutting feed, though they differ in their chamfer geometry:
- Form A Taps (DIN 371 / 376) feature an extended chamfer lead (6–8 threads). This geometry ensures the smoothest possible entry into the hole and evenly distributes cutting loads across the teeth. Form A is optimal for deep through-holes and machining ductile or gummy materials where a gentle, gradual start is critical.
- Form B Taps (DIN 371 / 376) feature a shorter chamfer lead (3.5–5 threads) with a specialized spiral point (gun nose) grind. The spiral point actively drives chips forward ahead of the cutting action, completely preventing chip packing in the flutes. This makes Form B the ideal choice for high-speed batch production on CNC machines.
Key Advantages of Volkel HSS-E Form A / B Taps
- Clean Thread Profile: Precision profile grinding guarantees compliance with ISO 2 (6H) tolerance class.
- Extended Tool Life: Cobalt alloying protects the cutting edge against thermal softening and micro-chipping under heavy loads.
- Reliable Chip Evacuation: Chips are pushed forward out of the through-hole, eliminating binding and tap breakage during spindle reversal.
- German Quality Control: Every Volkel tool undergoes multi-stage geometry and hardness inspection at manufacturing facilities in Germany.
The availability of both Form A and Form B geometries allows you to select the exact threading tool matched to your cutting parameters, hole depth, and workpiece material properties.